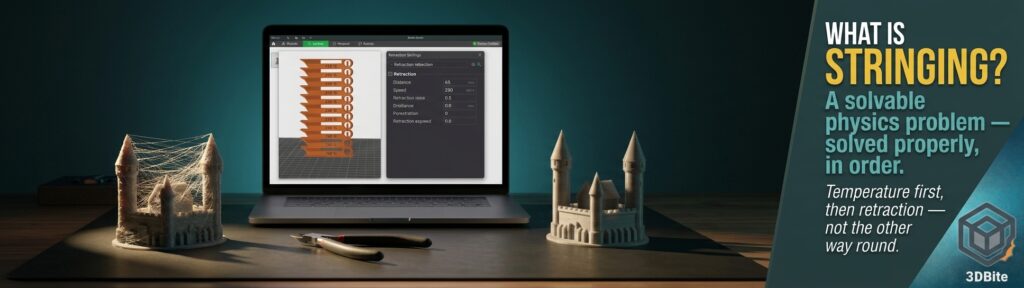
You pull a print off the bed and it looks like a spider has built a web between every tower, letter, and detail on the model. That is stringing — thin plastic hairs stretched between features that should have nothing connecting them — and it is one of the most common print quality complaints in this entire hobby, right behind bed adhesion failures. The good news, and it is genuinely good news, is that stringing is a solvable physics problem rather than a mystery. Molten plastic under pressure oozes out of the nozzle during travel moves. Counter that pressure properly and stringing disappears. This post works through exactly how, in the order that actually gets you to a clean result fastest.
What is actually happening
Stringing happens when the nozzle moves from one printed feature to another across open space — a travel move — and molten filament leaks out of the nozzle tip during that journey rather than staying contained. The leaked plastic stretches into a thin strand as the nozzle moves away, and that strand cools and solidifies mid-air, leaving a fine hair connecting two points that were never meant to be joined. It is happening because the melt zone inside the hotend is under pressure, and unless something actively relieves that pressure before the travel move begins, gravity and residual nozzle pressure will push a small amount of plastic out regardless of how carefully everything else is tuned.
Fixing it properly means controlling four separate things at once: how much filament gets pulled back before a travel move (retraction distance), how fast it gets pulled back (retraction speed), how runny the filament actually is at the moment it travels (temperature), and how much time the nozzle spends exposed over open air in the first place (travel path and speed). Get all four roughly right together and stringing genuinely disappears rather than merely reducing to an acceptable level.
The order that actually works: temperature first, not retraction
This is the single most useful piece of sequencing advice across every source researched for this post, and it runs against the instinct most people have when stringing first appears — which is to immediately start cranking up retraction distance. Printing too hot is the number one cause of stringing that retraction adjustments alone will never fully fix. If the filament is genuinely too fluid at the printing temperature you have set, it will ooze during every single travel move regardless of how aggressively you retract beforehand, because retraction only pulls back what is already in the nozzle — it does nothing to change how runny the remaining plastic at the tip actually is.
The correct diagnostic tool here is a temperature tower — a test print that changes nozzle temperature at set height intervals through a single job, letting you see the stringing behaviour at multiple temperatures on one print rather than running separate full prints for each guess. gaaZolee’s temperature tower model, available on both Printables and Thingiverse, is the standard reference model used across the community for this specific test. Print across a sensible range for PLA — 190°C to 220°C in 5°C increments is the commonly used span — and identify the lowest segment that still shows good layer adhesion with no extruder skipping or under-extrusion. That lowest clean segment is your target temperature. For most PLA+, this typically lands around 200-205°C. For PETG, the equivalent target usually sits around 230-240°C, noticeably below the 240-250°C that many filament spool labels print as their recommended range — PETG in particular bonds strongly even 15°C below its labelled “recommended” temperature, and printing at the label’s upper end is a common and avoidable cause of unnecessary stringing on this specific material.
Every 5°C reduction genuinely reduces oozing at travel moves — this is the single highest-leverage adjustment available before touching retraction at all, and skipping this step and going straight to retraction tuning is the reason a lot of stringing troubleshooting sessions take far longer than they need to.
Retraction distance and speed: the second lever
Once temperature is dialled to the lowest clean value, retraction is where the remaining stringing gets cleaned up. Retraction pulls filament backward through the nozzle just before a travel move begins, relieving the pressure in the melt zone so there is nothing left to ooze out while the nozzle is crossing open air. If the nozzle genuinely is not oozing, it cannot string — that is the entire logic behind the setting.
The specific starting values differ meaningfully by extruder architecture, and getting this distinction right matters. Bowden extruders — where the extruder motor sits away from the hotend and pushes filament through a long PTFE tube — need considerably more retraction distance to compensate for the tube’s inherent flex and the greater distance the pressure has to travel: a starting point of 5-6mm retraction distance at roughly 45mm/s retraction speed is the commonly cited range. Direct-drive extruders — which is what the A1 and A2L both use, with the extruder motor mounted right at the toolhead — need dramatically less: typically 0.4-1.0mm is enough, because the short, rigid path from the extruder gear to the nozzle transmits pressure changes far more immediately than a long Bowden tube ever could. Using Bowden-appropriate retraction values on a direct-drive machine is a common and avoidable overcorrection that can introduce its own problems — under-extrusion at the start of the next feature, and unnecessary wear on the extruder gear from excessive back-and-forth motion.
Retraction distance too low and stringing persists because there was not enough pull-back to relieve the pressure. Retraction distance too high risks jamming or clogging over time, and can slow the print down unnecessarily as the extruder spends more time retracting and re-priming than it needs to. The sensible approach is small, incremental adjustments — moving 0.1-0.2mm at a time on a direct-drive machine, testing on a small print between each change, rather than making one large jump and hoping it lands correctly.
Retraction speed interacts with distance rather than being independent of it. A retraction that happens too slowly gives the melt zone time to partially re-pressurise even as it is being pulled back, reducing the effective benefit of the retraction distance you have set. Most default profiles set retraction speed reasonably aggressively already, and this is generally the setting worth leaving close to default while distance does most of the tuning work — unless stringing genuinely persists after distance has been dialled in carefully.
Where to actually find these settings
In Bambu Studio: retraction distance and speed live under Printer Settings → Extruder (per-filament values can also be overridden in the filament profile itself under the Advanced tab if a specific spool needs different treatment from your general default). In OrcaSlicer: the same values sit under Printer Settings → Extruder 1, with the same per-filament override capability. Both slicers apply retraction on a per-filament-profile basis by default, which is worth remembering if you have several named, calibrated profiles as covered in the calibration routine post — a retraction fix applied to the wrong profile will not show up on the material you are actually testing.
Coasting and Wipe: the finishing touches
Two additional settings address the specific moment right at the end of an extrusion move, before retraction even begins, and they are worth knowing about once temperature and retraction have already done most of the work.
Coasting stops active extrusion slightly before the actual end of a printed line, letting the residual pressure already built up in the melt zone finish depositing that last small stretch of material rather than the extruder continuing to actively push right up to the very end. This uses up the pressure that would otherwise still be present at the moment retraction begins, meaning there is less residual pressure left to potentially ooze. A commonly cited starting coasting volume for PLA is around 0.064mm³, increasing to roughly 0.1mm³ if stringing persists after enabling it. Both Bambu Studio and OrcaSlicer expose this under the Advanced section of Process settings, sometimes labelled simply as Coasting distance or Coasting volume depending on version.
Wipe on retraction tells the nozzle to travel a short distance across the already-printed surface at the moment retraction begins, rather than lifting straight off cleanly. This has the effect of dragging any small amount of residual ooze across a surface that is about to be covered or is otherwise unobtrusive, rather than leaving it exposed and stringing visibly during the subsequent travel move. In Bambu Studio and OrcaSlicer this sits in the Seam section of Process settings, closely related to the Wipe on Loops setting covered in the Z-seam guide, since both settings are using the same underlying wipe mechanism for slightly different purposes.
Travel path: reducing the exposure rather than just managing the ooze
Everything above is about controlling how much plastic leaks during a travel move. A separate and complementary strategy is simply reducing how much time the nozzle spends exposed over open air in the first place, since less exposure time means less opportunity for stringing regardless of how well-tuned everything else is.
The one cause that no amount of settings tuning will fix
This connects directly to the filament drying post and deserves repeating clearly here rather than being treated as a footnote. Wet filament strings regardless of how carefully retraction and temperature have been calibrated, because the moisture trapped inside the polymer is turning to steam inside the hotend and creating intermittent pressure spikes of its own — spikes that push filament out during travel moves independently of any setting you have configured. If you hear popping or crackling sounds during printing while you are also seeing persistent stringing that settings adjustments are not resolving, the filament is wet, and no amount of further retraction or temperature tuning will fix a moisture problem. Dry the spool first, using the guidance in the drying post, and reassess stringing behaviour only after that variable has genuinely been ruled out — otherwise you risk chasing settings changes indefinitely against a problem that settings were never going to solve.
The material-specific reality
PLA is relatively forgiving and is where most people’s stringing troubleshooting resolves quickly and permanently once temperature and retraction are dialled in properly. PETG is more consistently difficult — its lower melt viscosity at typical printing temperatures means it oozes more readily than PLA even when both are printed within their respective recommended ranges, which is why PETG has a genuine reputation across the community as the stringier material by default rather than as a sign anything is wrong with your specific setup. The fix for PETG specifically leans harder on the temperature reduction than PLA typically needs — printing at the lower end of PETG’s range, combined with slightly more generous retraction than PLA would need on the same machine, is the combination that resolves most PETG stringing complaints.
TPU deserves its own specific mention because stringing on flexible filament is a genuinely harder problem than on rigid materials — the same softness that makes TPU flexible also makes it resist the sharp, clean retraction pull that rigid filaments accept easily, since a soft filament can compress and absorb the retraction motion rather than actually withdrawing cleanly from the melt zone. The TPU grades post covers the broader printing challenges by hardness grade, and the stringing-specific implication is that TPU generally needs a slower, more deliberate retraction approach than rigid filaments — aggressive fast retraction on soft TPU tends to produce inconsistent results rather than cleanly reducing stringing the way the same aggressive setting would on PLA.
The order to actually work through this in
Rather than adjusting everything simultaneously and losing track of what actually fixed the problem, work through these in sequence: confirm the filament is dry first, since this rules out the one cause settings cannot fix. Run a temperature tower and find the lowest clean printing temperature for the specific filament in use. Adjust retraction distance in small increments appropriate to your extruder type — 0.4-1.0mm for direct-drive machines like the A1 and A2L, considerably more for Bowden setups. Enable Coasting and Wipe if stringing persists after temperature and retraction are both dialled in. And finally, consider travel path optimisation — combing or its equivalent — specifically for display pieces where any residual stringing on visible outer surfaces genuinely matters more than the small print time penalty the setting introduces.
Done in that order, most stringing problems resolve within one or two test prints rather than the extended, frustrating trial-and-error process that adjusting everything at once tends to produce. Stringing genuinely is a solvable physics problem, and the physics behaves exactly the same way every time — which means, once you understand the mechanism properly, it stops being a mystery and becomes just another calibration step.
Really clear on the sequencing — temperature first, then retraction — and that matched what I kept getting wrong on PETG towers. Cranking retraction while the nozzle was still 10–15°C too hot just made the strings thinner, not gone. Wet filament was the other silent culprit: once moisture turns to steam in the hotend, wipe/coast/combing will not save you until the spool is dry. Even after settings are dialed in, models with lots of tiny islands and long open travels still string a bit no matter how tidy the profile is. Getting the mesh itself cleaner with fewer micro-islands and shorter air moves has cut more hairs for us than another retraction tweak, which is what we work on at luphra.com.