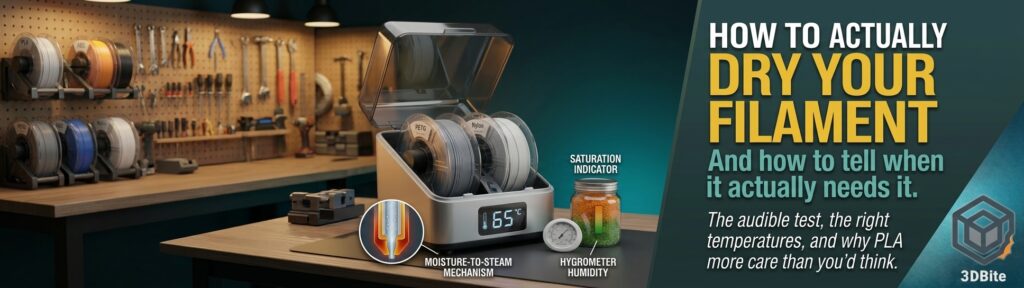
Wet filament is the invisible print killer this site keeps circling back to without ever giving it the dedicated treatment it deserves — it came up in the fumes post, the cheap filament post, the drybox build, and the hot weather post, always as a contributing factor to something else rather than the main subject. It earns its own post because the underlying mechanism is genuinely simple, the symptoms are genuinely diagnosable if you know what to listen for, and the fix is genuinely just time, heat, and airflow done correctly rather than anything complicated.
Why filament absorbs water in the first place
Most 3D printing filaments are hygroscopic — a term that simply means the polymer chemistry allows water molecules from the surrounding air to bond to the material rather than sit on the surface. This is not a manufacturing defect or a sign of poor quality. It is a basic chemical property of the plastics involved, and it applies to some degree to every common filament, just at wildly different rates depending on the specific polymer.
PLA absorbs slowly. In a very humid environment — 70-80% relative humidity — a spool might start showing measurable effects within a week or so. In a genuinely dry room, it can take weeks or months. PETG and TPU absorb noticeably faster than PLA and can become print-affecting within days in a humid room rather than weeks. Nylon and PA-CF are in an entirely different category — absorbing 1-2% of their own weight in moisture within 24 hours of room-humidity exposure, which is genuinely sponge-like behaviour rather than a gradual process, and can start showing negative effects within a day or two in humid conditions. This scaling is the reason this post treats “how long can I leave this spool out” as a material-specific question rather than a single universal answer.
What actually happens inside the nozzle
This is worth understanding properly because it explains every symptom that follows. When wet filament enters the hotend at printing temperature — 200-260°C depending on material — the water trapped within the polymer flashes instantly to steam. That steam does not politely diffuse away; it forms a bubble that bursts out through the molten plastic at the nozzle tip, disrupting the smooth extrusion flow and leaving a small void or defect exactly where the steam escaped. The popping or crackling sound you sometimes hear during printing is, quite literally, a tiny steam explosion happening at the nozzle in real time. It is the same physics as a kettle boiling, scaled down to microscopic volumes and happening continuously as wet filament feeds through.
The symptoms, and how confident each one lets you be
Several genuinely different symptoms all trace back to moisture, but they carry different levels of diagnostic certainty, and it is worth being honest about which ones are proof and which are merely suggestive.
The audible test is the closest thing to a definitive answer. Heat the nozzle to your normal printing temperature, then use manual extrusion control to push filament through slowly while listening closely. Popping, crackling, or a faint hissing sound during that slow extrusion is steam escaping in the melt zone, and it is about as close to a clear positive result as this diagnosis gets. If you hear it, the filament needs drying — this is not a symptom that has an alternative, non-moisture explanation.
Visual and print-quality symptoms are suggestive but not proof on their ownnozzle wear post, or an incorrect slicer profile. Before running a drying cycle on the strength of these symptoms alone, it is worth confirming the spool feeds freely, the nozzle is not partially obstructed, and the correct material profile is actually loaded in the slicer. A print that has suddenly gone rough or under-extruded can look identical whether the cause is moisture or a mechanical problem, and treating every quality issue as automatically a drying problem wastes time on cycles that were never going to fix the actual cause.
Reduced mechanical strength is the symptom that matters most and is hardest to see coming. Wet filament can produce parts that are measurably weaker — some sources put this at 20-50% reduced strength — without necessarily showing any obvious surface defect at all. This is the genuinely concerning version of the problem: a print that looks completely fine but fails under load it should have handled easily, because the steam voids weakened the layer bonding internally in a way that is not visible from outside. This is the strongest argument for treating drying as a habit for functional and load-bearing prints specifically, rather than only reaching for the dryer once a visible defect has already appeared.
Exposure history is a legitimate trigger on its own. A spool that has spent a long time sitting open, or one loaded in the AMS Lite for an extended period as covered in the workflow costs post, is worth treating as a drying candidate even before any visible symptom appears — particularly for PETG, TPU, and nylon, where the timescale for meaningful absorption is short enough that waiting for symptoms means the print quality has already been compromised for a while before anyone noticed.
Do not make drying an automatic step for every spool
This is worth stating plainly against the instinct to just dry everything preventatively regardless of need. Running a full drying cycle on a fresh, properly sealed spool that has never shown a symptom is unnecessary electricity and time spent solving a problem that does not exist yet. The sensible approach is symptom-triggered for spools in regular rotation — dry when the audible test or a genuine print quality problem appears — combined with exposure-triggered drying specifically for anything that has sat open for a long period or lived in the AMS for an extended multi-colour project. Preventative drying on a schedule, rather than in response to an actual signal, is the wrong default for most filament in most conditions.
The temperatures and times, by material
The specific numbers below are conservative starting ranges gathered across multiple current guides rather than a single universal specification — pigments, fillers, specific polymer blends, and individual dryer accuracy all shift the ideal setting slightly, and the filament manufacturer’s own guidance, where published, takes priority over any generic table.
| Material | Drying temperature | Drying time | Notes |
|---|---|---|---|
| PLA | 45-50°C | 6-8 hours | PLA begins softening around 60-64°C — never push toward this range, or the spool fuses into a solid unusable puck |
| PETG | 60-65°C | 6 hours | Absorbs faster than PLA — worth drying more readily on exposure history alone |
| TPU | 50-70°C | 4-8 hours | Range varies more by specific Shore hardness grade than most materials — see the TPU grades post |
| ABS / ASA | 70-80°C | 4-8 hours | Higher tolerance for heat means less risk of accidentally softening the spool during drying |
| Nylon / PA-CF | 80-95°C | 8-16 hours | The most demanding material to dry properly — absorbs fastest, needs the longest and hottest cycle |
Wet filament is still the silent culprit behind half the “mystery” stringing and pop-pop bubbles I see. PLA can limp along slightly damp, but nylon and PETG punish you fast — weak layer bonds and a foggy surface are usually my tell before I even open the dryer. A food dehydrator at ~45–55°C for PLA (higher for nylon) plus a weigh-every-hour check until the spool stops dropping grams beats guessing oven times. When it finally prints clean with no steam hiss from the nozzle, bag it with fresh desiccant the same day or it just reabsorbs overnight.